

Wolong EC Fan Energy Efficiency Retrofit Case | Yichang Ziquan Beverage Industry Co., Ltd. | Permanent Magnet Direct-Drive EC Fan Retrofit for Workshop Air Handling Units
[Project Background] A total of 2 workshop air handling units (AHUs) with retrofit potential were identified across Line 1 and Line 2 at Ziquan Beverage Industry Co., Ltd. The Line 1 AHU features a motor power of 18.5kW, an airflow rate of 35000m m³/h, and a total pressure of 1150Pa. The Line 2 AHU has a motor power of 30 kW, an airflow rate of 40000m m³/h, and both lines operate approximately 7920 hours annually. Originally, the AHU drive systems utilized standard impellers, belt drives, and three-phase asynchronous motors. [Pre-Retrofit Issues] Belt drives suffer from slip losses, lag losses, air resistance, and bearing friction, resulting in a transmission efficiency of only about 90%. They also generate high vibration and noise, causing frequent wear and damage to belts and fan bearings, leading to high failure rates and requiring dedicated staff for regular inspections. Three-phase asynchronous motors typically operate at efficiencies between 77% and 91%, with significant efficiency drops under low loads. As service life increases, excessive heating further reduces efficiency, keeping the entire fan system operating in a low-efficiency zone for extended periods. [Retrofit Solution] The project replaces the original supply air combination with a Wolong permanent magnet rotor synchronous motor direct drive, an intelligent variable frequency drive (VFD) system, and a high-efficiency EC fan system. The configuration includes 6 high-static-pressure EC fans, 1 batches of fan frames and accessories, and 2 control cabinets (Equipment Nameplate: ATB EC Fan Control Cabinet, Model ATB-A-EC-A-S-M-1-B, Rated Voltage 380VAC 50Hz, Protection Rating IP42, manufactured by Wolong (Shanghai) Energy Saving Technology Co., Ltd. in 2025 12). The EC motor features integrated drive and control design, utilizing permanent magnet circuit simulation and high-thermal-conductivity plastic encapsulation to prevent bearing electrical erosion. The energy-saving drive controller employs DFC software control algorithms and film capacitor technology, supporting interconnection, group control, and remote monitoring. The control system integrates with existing infrastructure, maintaining current control methods. The HMI main interface displays power, speed, current, load rate, and the operational status of each fan, while tracking cumulative operating hours and energy consumption. [Retrofit Results] Input power for the Line 1 AHU decreased from a measured 17.4kW to a designed 14.7kW, while Line 2 dropped from 21.9kW to 11.7kW. Based on an annual operation of 7920 hours and an electricity cost of 0.8 CNY/kWh, annual energy consumption was reduced from 311,256kWh to 209,088kWh, saving 102,168kWh annually with an energy savings rate of 32.8%. Total annual costs (including maintenance) decreased from 250,004 CNY to 167,270 CNY, saving approximately 82,734 CNY per year. On-site HMI measurements showed an operating power of 6.7 kW, speed of 1624r/min, current of 12.9 A, and load rate of 57.0%, with stable operation of the 5 fan group under centralized control. [Audit & Service] Energy audit is conducted by comparing hourly consumption over 72 hours under similar operating conditions before and after retrofitting. Acceptance is granted if saved energy W3=W1-W2 and energy savings rate =W3/W1 are achieved, and airflow/pressure meet pre-retrofit performance requirements. After-sales services include free maintenance and repair during the contract period, 7x24 rapid response, scheduled inspections, spare parts guarantee, and safety training.
ON-SITE GALLERY
Site Gallery
RESULTS
Transformation Results
SAVING RATE
Overall energy consumption reduction after retrofit
ENERGY COMPARE
Annual Energy Consumption Comparison (Unit: 10,000 kWh)
KEY METRICS
After retrofitting, the air handling unit operates at 67kW power, 1624r/min RPM, with a load rate of approximately 57%. 5 EC fans run in stable group control. Annual energy savings amount to 102,168kWh, reducing electricity costs by approximately 82,734 yuan annually, while significantly decreasing maintenance workload for belts and bearings.
Data Scope and Validation Source: The above metrics are derived from on-site measurements under identical operating conditions before and after the retrofit (comparing energy meter readings with equipment operation logs). The statistical period covers 30 consecutive days of full operation post-retrofit. Motor energy efficiency ratings follow GB 18613-2020 and IEC 60034-30-1, while product efficiency values are cited from the manufacturer's factory test reports. Actual results may vary based on load rate, annual operating hours, and specific operating conditions.
STRUCTURED LINKS
Related Products & Industries
Related ProductsCo2Item
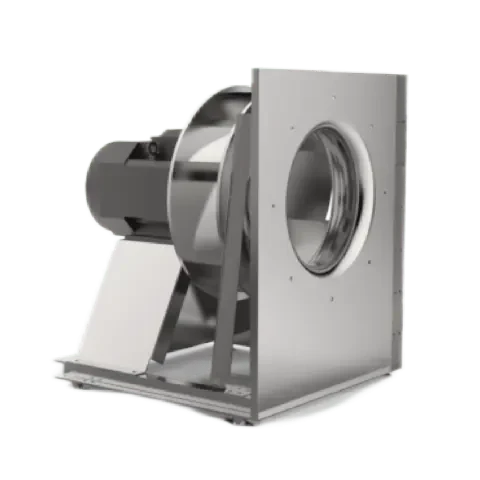
Pengke PLF Centrifugal Fan (EC/AC)
Pengke PLF Centrifugal Fan (EC/AC), direct-drive motor without volute, max airflow 120000m³/h, max pressure 4500Pa, max static efficiency 79%, max total efficiency 83%, impeller diameter 250mm–1250mm. Ideal for large industrial air handling units.
View Product Details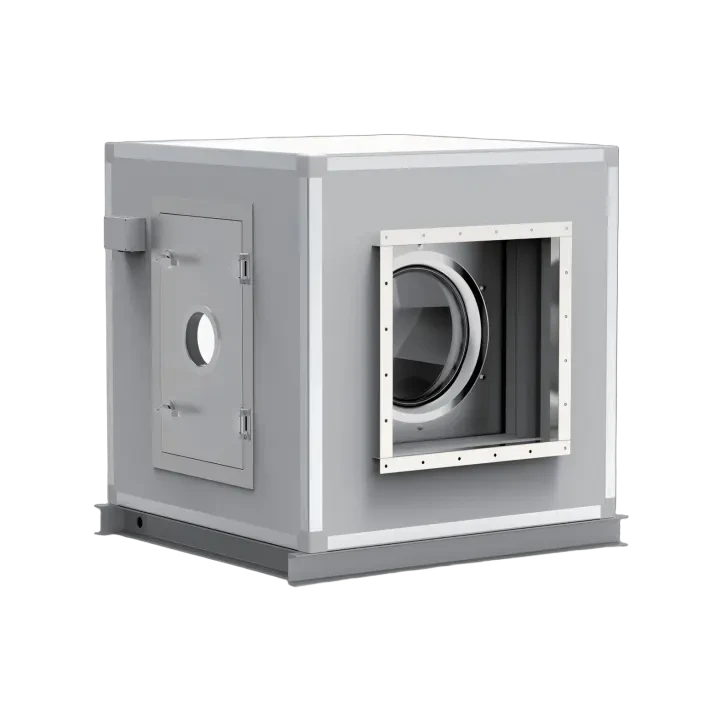
Pengke PLFB Centrifugal Supply and Exhaust Fan Unit (EC/AC)
PENGKE PLFB Centrifugal Supply and Exhaust Fan Unit (EC/AC) with quick-release housing design. Maximum airflow: 100000m³/h, maximum pressure: 4500Pa, peak static pressure efficiency: 79%, peak total pressure efficiency: 83%. Impeller diameter: 250mm–1250mm. Ideal for ducted supply/exhaust ventilation and server room air handling.
View Product DetailsRELATED
Products and Solutions in this Project

Belt Conveyor Drive Control
Belt Conveyor Drive and Control System Solution
Low-speed permanent magnet direct-drive system solutions for belt conveyors in mining, chemical, and building materials industries. The TYCP5 series low-speed permanent magnet motor drives the conveyor directly, eliminating intermediate components such as gearboxes, fluid couplings, and multi-stage pulleys. Paired with the WD200 high-performance vector frequency converter, ECC variable-frequency control cabinet, advanced PLC, wired/wireless integrated temperature-vibration sensors, and Wolong iMotorLinx Shunzhi Cloud industrial internet platform, it simplifies the transmission chain, improves efficiency, and enables real-time monitoring of operational status.

Permanent Magnet Drum Drive Control
Permanent Magnet Drum Drive Control System Solution
A permanent magnet electric drum direct-drive system solution for belt conveyors in mining, chemical, and building materials industries. Replacing traditional drive systems with gear reducers and asynchronous motors, the STY series permanent magnet direct-drive drums are paired with WD200 series high-performance universal variable frequency drives and energy feedback units, Wolong Shunyun IoT modules and PLCs, advanced wireless temperature-vibration integrated sensors, and the Wolong iMotorLinx Shunzhi Cloud industrial internet platform to achieve simplified transmission chains, S-curve smooth starts, precise speed-torque control, and energy recovery.
SOLUTIONS
Recommended related solutions

Food Industry Measurement and Control Solutions
Designed for food and beverage manufacturers, our hygienic measurement instruments and recording control systems meet EHEDG and FDA material standards across ten key dimensions: temperature, water quality analysis, pressure, flow, hygienic process connections, humidity, control, recording, monitoring, and automation visualization. These solutions ensure stable production operations and support full quality traceability requirements.

Brewing Industry Measurement and Control Solutions
An end-to-end automation system for temperature, pressure, pH, conductivity, and humidity monitoring and control, designed for malt and beer production. It covers all stages of malting (storage, steeping, germination, kilning) and brewing (mashing & lautering, boiling & cooling, fermentation storage, filtration, bottle cleaning, and CIP), ensuring consistent, repeatable brewing processes while reducing energy consumption.

Permanent Magnet Drum Drive Control System Solution
A permanent magnet electric drum direct-drive system solution for belt conveyors in mining, chemical, and building materials industries. Replacing traditional drive systems with gear reducers and asynchronous motors, the STY series permanent magnet direct-drive drums are paired with WD200 series high-performance universal variable frequency drives and energy feedback units, Wolong Shunyun IoT modules and PLCs, advanced wireless temperature-vibration integrated sensors, and the Wolong iMotorLinx Shunzhi Cloud industrial internet platform to achieve simplified transmission chains, S-curve smooth starts, precise speed-torque control, and energy recovery.
More Cases
View All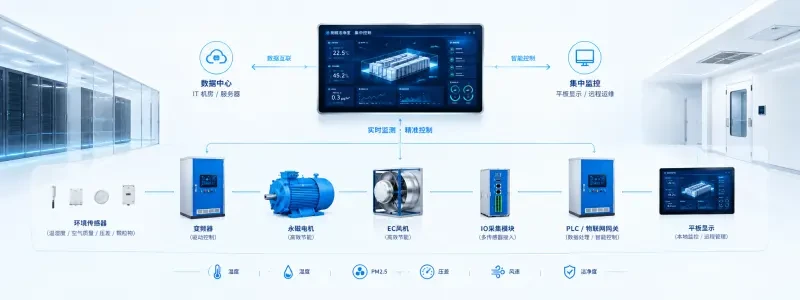
Panpu EC Permanent Magnet Fan Case | Cleanroom Operator | Energy-Saving Retrofit of Cleanroom Fan Clusters with On-Demand Speed Control
Replace traditional AC fan clusters with EC permanent magnet fans, and use differential pressure sensing to enable on-demand speed control for air supply, reducing energy consumption and noise in the cleanroom's ventilation system.
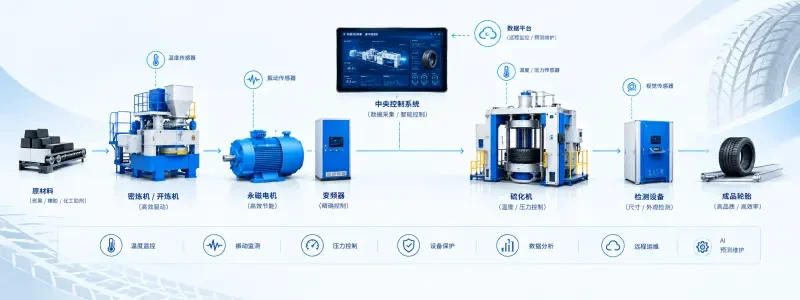
Panpu Permanent Magnet Direct Drive Motor Case: Kiri Chemical Rubber Tire Factory – Whole-Line Drive System Energy Efficiency Retrofit for Tire Production Line
Optimize the motor drive system across the entire tire production line, coordinate multi-device control to reduce overall energy consumption, and adapt to wheel control and molding processes. Help factories achieve energy savings, carbon reduction, and improved production efficiency.

28 0KW Permanent Magnet Motor + VFD Case Study | SCM Chemical Fiber | Large-Scale Process Equipment Retrofit for Energy Efficiency
Equipped with a 280kW permanent magnet motor and dedicated variable frequency drive (VFD), this integrated solution optimizes load performance, reduces energy consumption, and enhances operational stability. It delivers complete case study support to help large-scale process equipment achieve cost reduction and efficiency gains.
Looking for a motor and energy-saving solution tailored to your operating conditions?
Submit request. Our technical engineer will contact you within 1 business days.